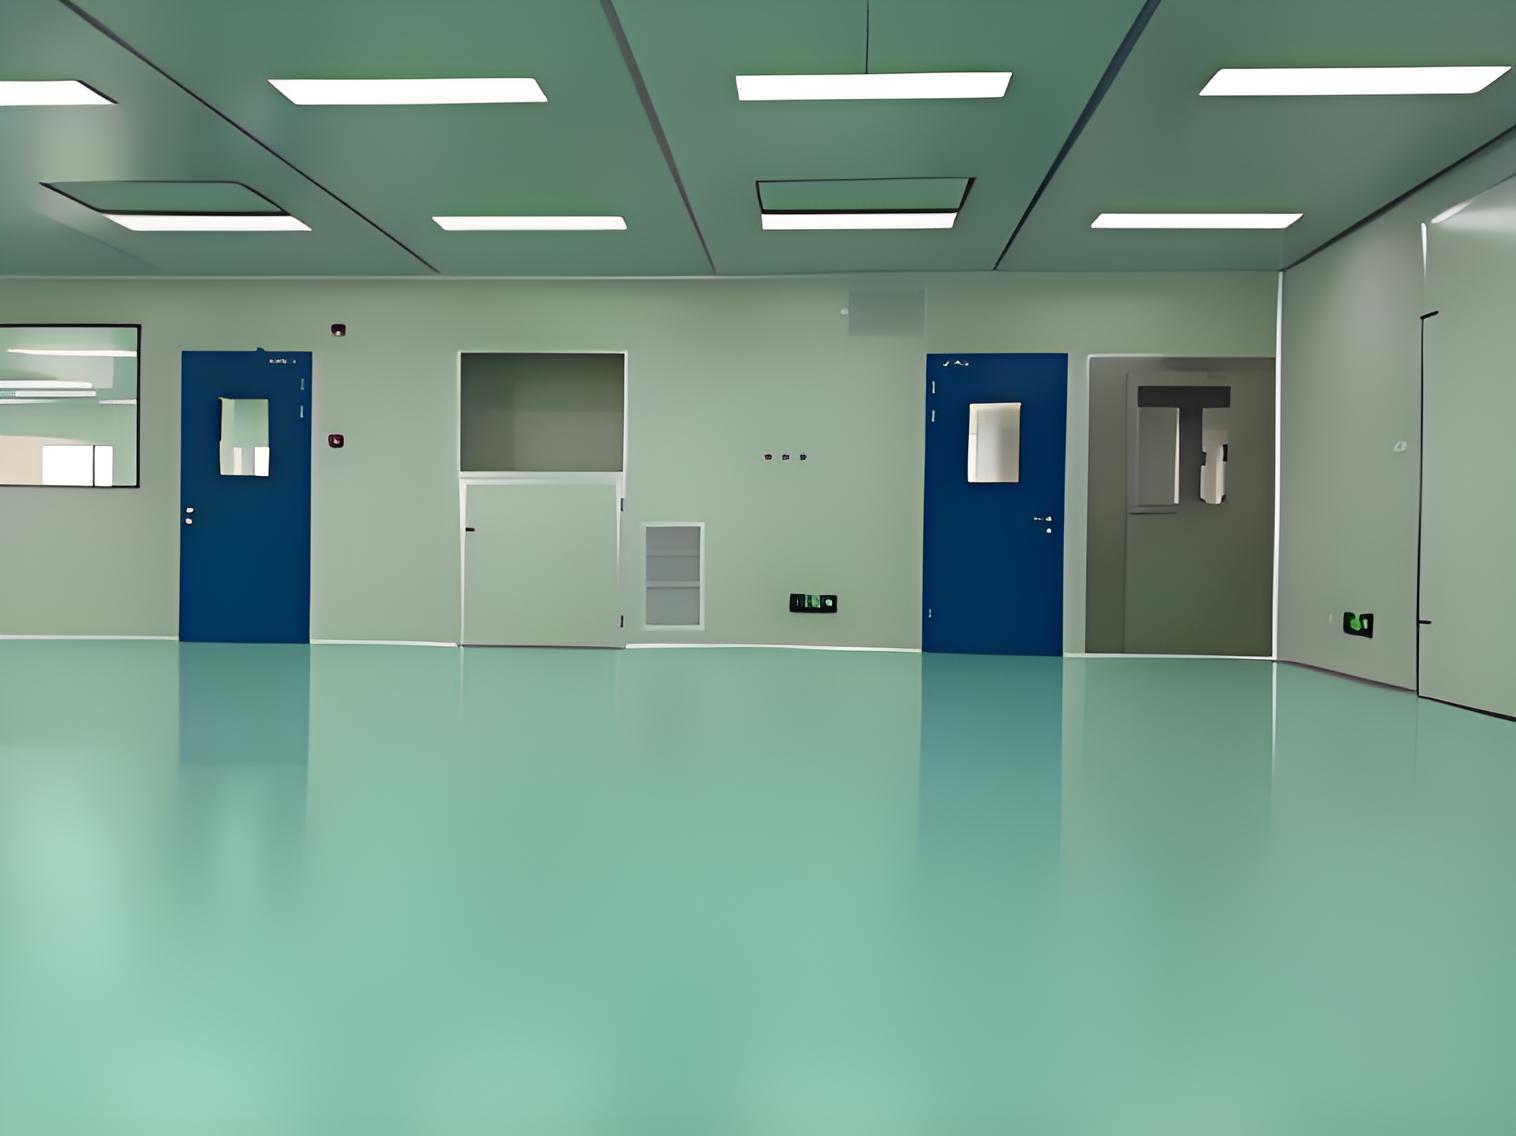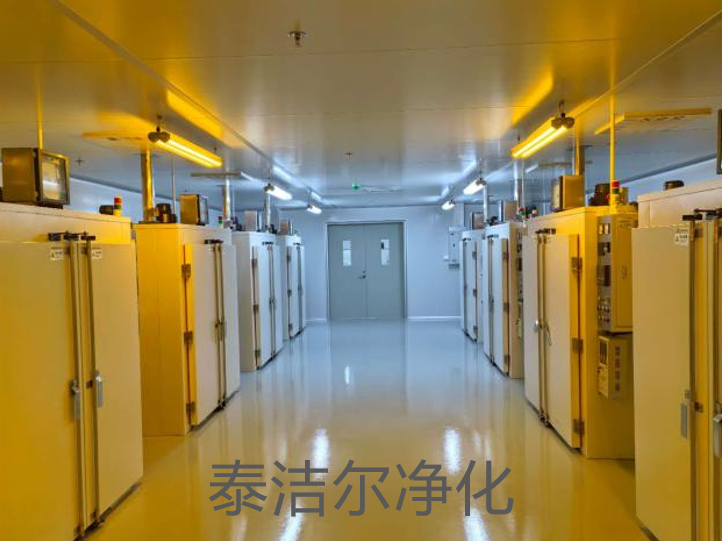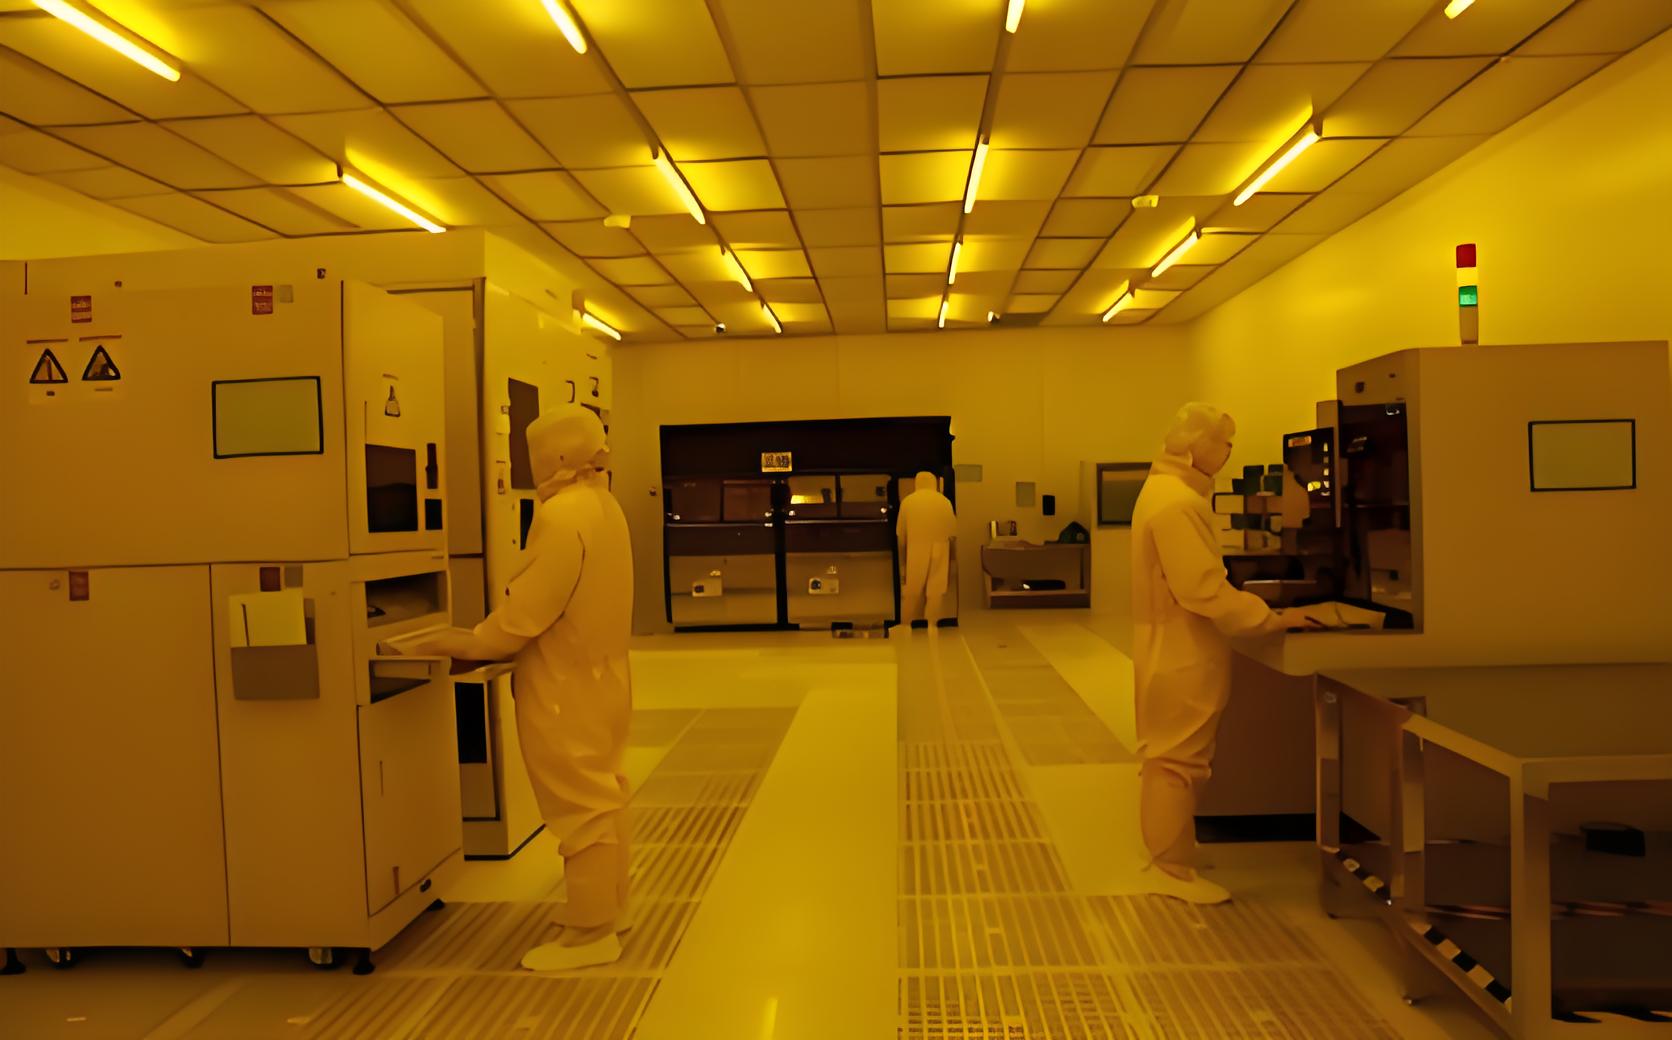

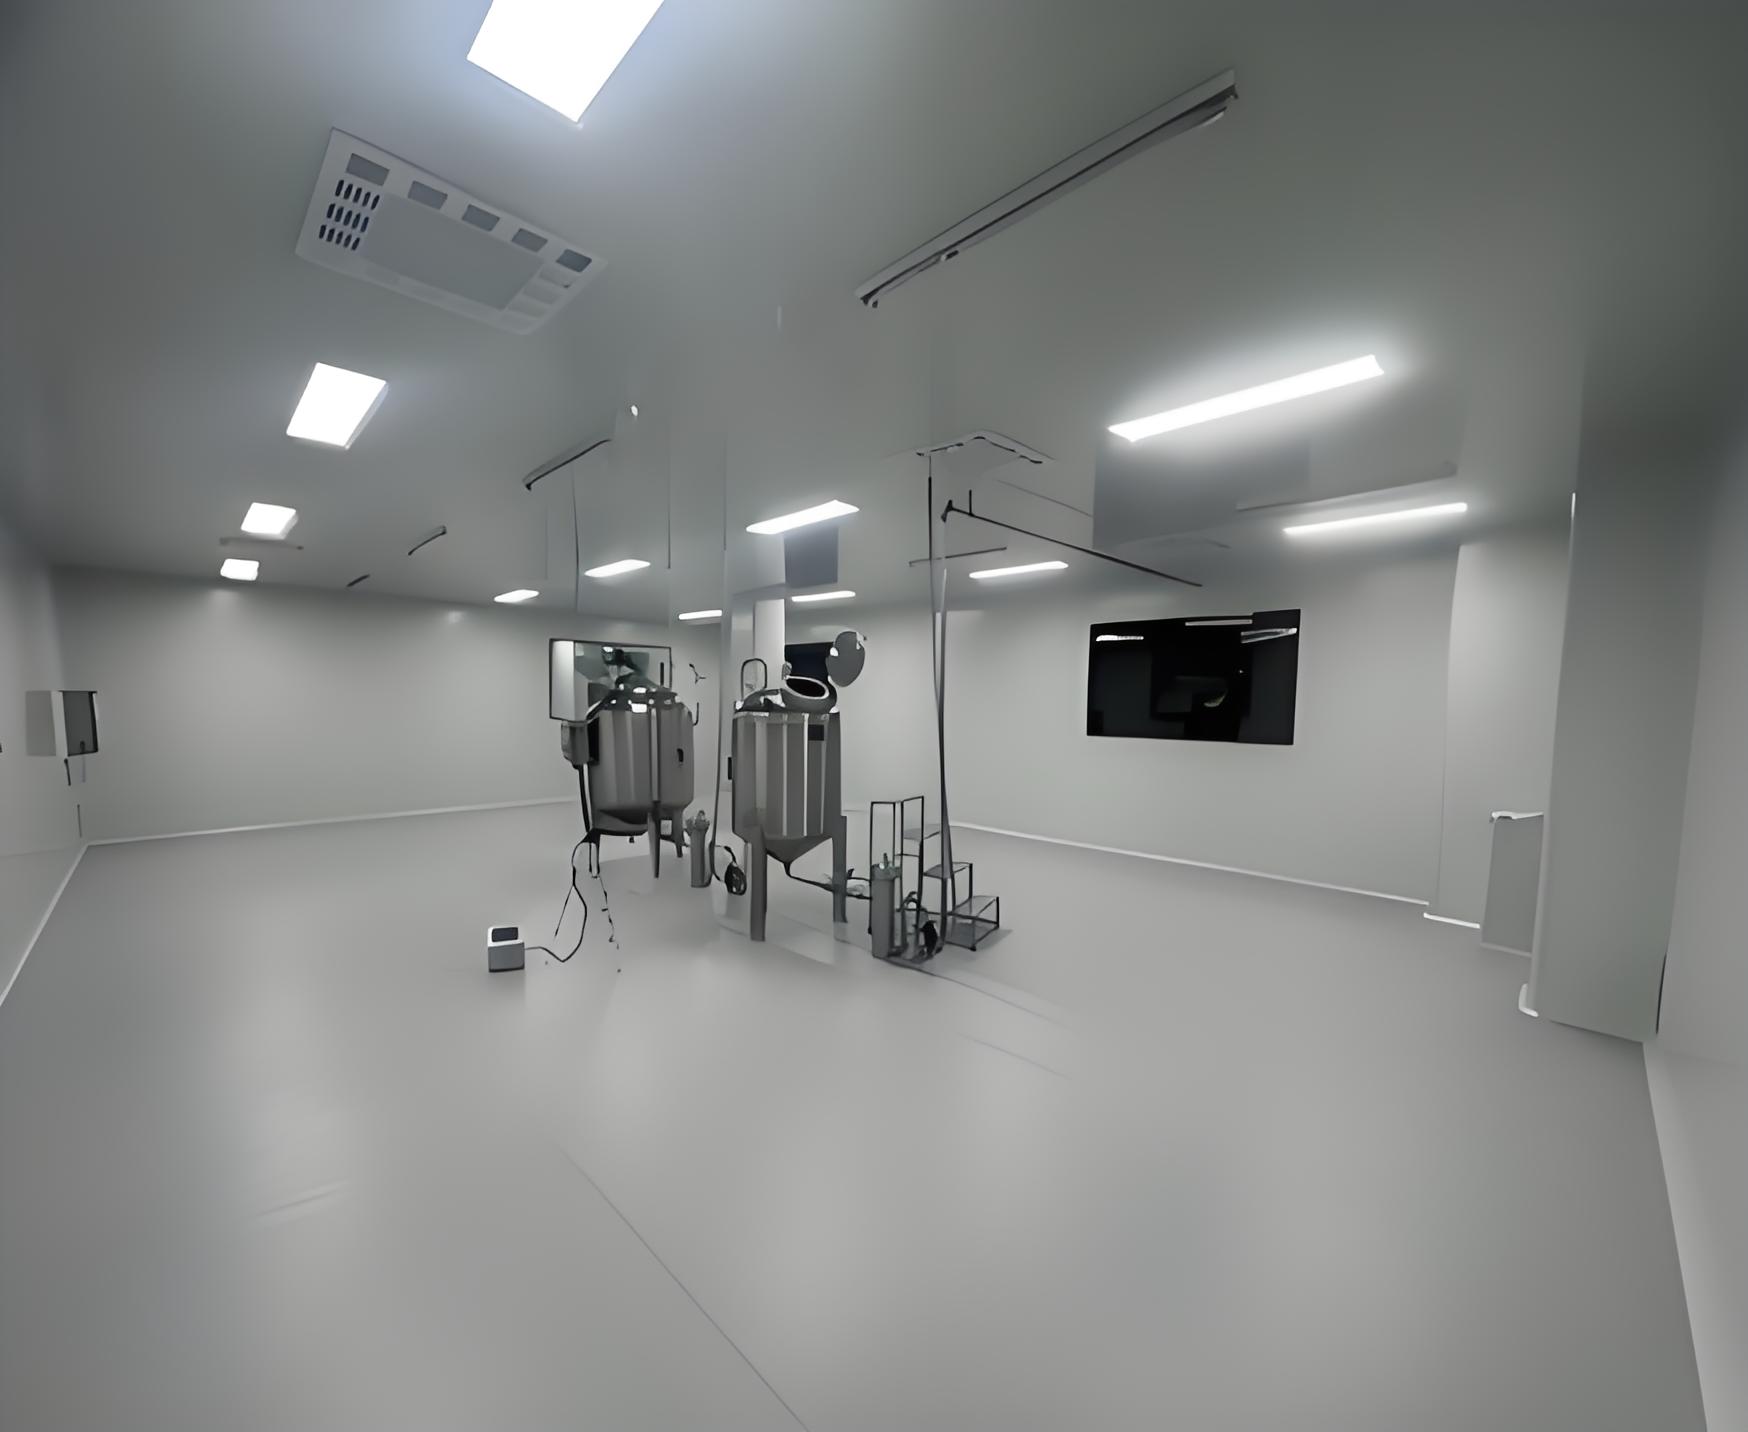
A cleanroom is an engineered space in which airborne particles, temperature, humidity, pressure, and airflow are controlled to protect products and processes. Getting the fundamentals right separates a reliable facility from an expensive room that never passes validation.
This guide covers classification standards, design principles, airflow strategies, qualification, and daily operating practice for modern controlled environments.
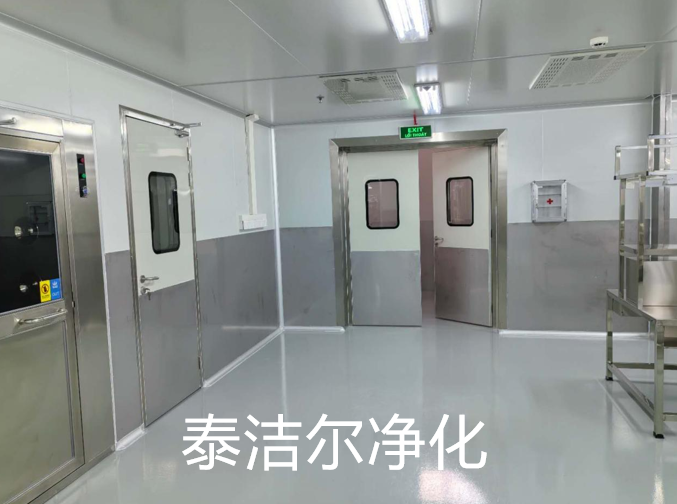
A cleanroom combines architectural sealing, filtered air supply, and strict operating discipline. Each element exists to keep particle counts within agreed limits.
The consequences of poor control vary by sector:
Semiconductor lines lose yield when sub-micron particles settle on wafers.
Pharmaceutical batches risk contamination and rejection.
Medical devices may fail sterility assurance requirements.
Cleanliness is a measurable engineering outcome, not a cosmetic feature of the building.
Classification defines how much contamination is allowed in a given volume of air. Most projects reference one or two standards, depending on the market served.
ISO 14644-1 grades rooms from ISO 1, the strictest, to ISO 9. The grade is set by the maximum permitted number of particles at defined sizes per cubic metre.
ISO 5 corresponds roughly to the former US Class 100.
ISO 7 corresponds roughly to Class 10,000.
ISO 8 corresponds roughly to Class 100,000.
Pharmaceutical manufacturing uses Grades A, B, C, and D. Grade A applies to high-risk operations such as aseptic filling, and it is normally achieved inside a localized unidirectional airflow zone.
This US standard was withdrawn in 2001 but still appears on legacy drawings and contracts. Always confirm which edition a specification references before quoting or building.
The airflow pattern must match both the process risk and the equipment footprint.
Unidirectional flow supplies filtered air across the entire work zone and suits critical operations.
Non-unidirectional flow relies on dilution and mixing, which is cost-effective for lower grades.
Mixed systems protect islands of high risk inside a larger background area.
Differential pressure keeps contamination moving from cleaner to less clean areas, never the reverse. Typical cascades run around 10 to 15 Pa between adjacent zones.
Direction depends on the product. Aseptic suites usually run positive, while containment laboratories handling hazardous materials often run negative.
Terminal HEPA filters perform the final particle removal step. ULPA filters are specified where sub-micron control is critical, such as advanced semiconductor lines.
Pre-filters and intermediate filters protect the terminal stage and extend its service life, which lowers long-term operating cost.
Non-shedding wall panels with smooth, cleanable joints.
Coved floor-to-wall connections to prevent soil traps.
Flush-mounted lighting and sealed service penetrations.
Surface finishes that tolerate the validated cleaning agents.
Air handling units deliver filtered air at the correct volume, temperature, and humidity. Air change rates typically range from around 20 per hour for ISO 8 up to several hundred for the strictest ISO 5 zones.
Energy use is often the largest operating cost in a controlled facility. Good design balances air change rate against actual contamination risk instead of applying maximum rates everywhere.
Monitoring should cover at least the following:
Particle counts at defined critical locations.
Room-to-room differential pressure.
Temperature, humidity, and filter loading.
Recovery time after a simulated contamination event.
Commissioning proves that the installed system works as designed. Qualification then documents that it meets the user requirement specification.
Installation qualification checks components, drawings, and materials.
Operational qualification tests airflow, pressure, and control logic.
Performance qualification confirms performance under routine production conditions.
Particle count testing, filter integrity testing, and airflow visualization should be repeated at defined intervals after handover, and after any significant modification.
People are the largest contamination source in any controlled space. Procedures matter more than equipment upgrades in most audits.
Use a documented gowning sequence, observed by a trained colleague during qualification.
Provide dedicated garments and define change frequency limits.
Restrict jewellery, cosmetics, and personal items.
Cleaning agents must be validated for the surface types in use. Maintenance work should follow a controlled permit process to avoid unnecessary particle release.
Training records, cleaning logs, and deviation reports are usually the first documents an auditor requests.
Requirements differ sharply between sectors, which is why specification review comes before layout design.
Pharmaceuticals: aseptic processing, sterility assurance, and data integrity.
Semiconductors: sub-micron particle control and chemical contamination limits.
Medical devices: implant manufacturing and sterile packaging.
Food and beverage: shelf-life extension and microbial control.
Electronics and optics: surface cleanliness and static control.
Each sector brings its own audit expectations, so early alignment with the regulator or certifying body saves rework later.
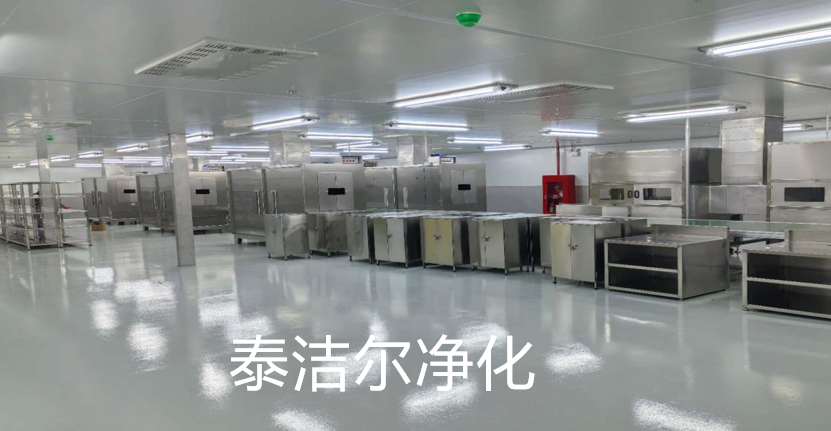
Design decisions made early are difficult and costly to reverse. A partner who understands both the standards and the practical construction sequence reduces that risk.
TAI JIE ER provides cleanroom engineering, partition systems, and controlled environment solutions for pharmaceutical, electronics, and healthcare projects. The team supports classification planning, layout design, and on-site installation.
Engaging specialists early clarifies airflow, pressure zoning, and material selection before drawings are frozen. TAI JIE ER also prepares the documentation packages needed for qualification and regulatory audits.
A1: ISO 7 permits fewer particles at each measured size than ISO 8. ISO 7 is often used for clean zones around critical processes, while ISO 8 typically covers background support areas.
A2: Most facilities are tested at least every 12 months, and some regulated operations require six-month intervals. Recertification is also required after major modifications or filter replacement.
A3: The rate depends on the target grade, occupancy, and process emissions. Typical values run from about 20 air changes per hour for ISO 8 up to several hundred for the strictest zones.
A4: A gowning room is usually positive to the corridor and negative to the cleaner production area. This arrangement keeps contamination from entering the critical zone.
A5: Often yes, provided there is enough ceiling space for air handling and filtration. A structural and HVAC survey should come before any design work begins.
A6: Leaks at service penetrations, door seals, and ceiling joints are frequent causes. Inadequate airflow balancing and incomplete documentation also appear regularly.
A well-run cleanroom is the product of clear specifications, correct airflow design, and disciplined daily operation. Standards define the target, but construction quality and procedure control determine whether that target is met year after year.
Review classification requirements at the start of the project, document every design decision, and validate against measurable criteria. That approach keeps performance predictable and keeps audits straightforward.
For projects that need engineering support from concept through handover, TAI JIE ER offers practical assistance with layout, materials, and installation planning.